AI for Predictive Maintenance: Analyzing Manufacturing Sensor Data in 2026

Explore how manufacturing teams use ERPNow dashboards to analyze sensor telemetry, vibration data, and equipment failure modes for condition-based planning and predictive maintenance services.

6 Real WorkflowsUpdated with every UGC run
Rachel Hu

Rachel Hu

AI Researcher at UC Berkeley


Executive Summary

Modern manufacturing relies on precise sensor analysis to prevent unplanned downtime. ERPNow turns operating parameters and vibration data into evidence that engineers can review before updating maintenance records in cloud based ERP software. Reliability teams retain the detailed signal work, and enterprise resource management software receives a clearer explanation behind each alert.

  • Transition from calendar-based to condition-based maintenance using sensor thresholds.
  • Detect tool failure signatures by analyzing high-frequency accelerometer data.
  • Eliminate manual reporting errors by unifying narrative summaries and visualizations.

6+ Real-World Listings

1.Condition-Based Maintenance Parameter Thresholds

Data table · 2026

A manufacturing reliability team faced a costly problem: calendar-based maintenance schedules left high-utilization lines vulnerable to unplanned stoppages because they ignored actual equipment condition. To build a condition-based plan, a reliability engineer analyzed 9,652 baseline events against 348 observed failures, correlating specific breakdown modes with median thresholds for torque, rotational speed, and temperature gap. The dashboard isolated defensible trigger rules. It proved that heat dissipation failures consistently occur at an 8.3 K median temperature gap and 52.4 Nm torque.

What it shows:

How correlating sensor data with failure logs gives maintenance teams the defensible parameter thresholds needed to transition to condition-based scheduling.

#reliability-engineering#condition-based-maintenance#sensor-thresholds

2.CNC Tool Failure Signature Detection

Scatter plot · 2026

A precision machining facility faced a costly problem: CNC tool failures often looked normal to the naked eye, so anomalous cycles were caught only after expensive parts had been scrapped. To move from reactive to proactive monitoring, a process engineer analyzed accelerometer data, using a scatter plot to correlate maximum amplitude with Y-axis kurtosis and a bar chart to track cycle duration. Bad cycles showed a sharp drop to negative kurtosis and shortened from roughly 60,000 to 40,000 data points, providing a clear statistical signature of tool disengagement.

What it shows:

How isolating statistical signatures in accelerometer data with ERPNow reveals tool disengagement so process engineers can intervene before scrapping precision parts.

#cnc-machining#accelerometer-data#kurtosis-analysis

3.Variance-Based Vibration Condition Monitoring

Box plots · 2026

A precision machining facility faced a common monitoring problem: simple peak-amplitude vibration thresholds caught catastrophic tool breaks. Subtle, low-amplitude process drift could still produce scrapped parts before those alarms fired. To find a reliable signal, a CNC process engineer used automated feature extraction to batch-process accelerometer data, comparing healthy and faulty runs with box-and-strip plots and log-scaled variance distributions. The analysis located fault signatures in distributional stability. Healthy X-axis Kurtosis clustered tightly around 6.19, and faulty Z-axis RMS variance exploded with a 92.08x spread ratio.

What it shows:

How automated feature extraction from vibration data enables process engineers to implement reliable, variance-based condition monitoring with confidence.

#vibration-analysis#variance-monitoring#feature-extraction

4.Multi-Axis Structural Vibration Diagnosis

Heatmap · 2026

A precision machining team faced a dangerous blind spot: overall amplitude can remain near normal during a fault, leaving standard RMS alarms unable to flag the run. Naive threshold comparisons could therefore clear faulty production as normal. A CNC process engineer diagnosed the recurring issue by comparing multi-axis features across nominal and anomalous states with a percent-change heatmap and grouped bar charts. The view revealed a counter-intuitive signal collapse: Y-axis crest factor and kurtosis fell by -63.8% and -74.3%, proving the fault was structurally quieter despite a slight 17.9% RMS increase.

What it shows:

How analyzing multi-axis feature collapses in sensor data helps engineering teams diagnose structural faults that standard amplitude alarms miss.

#structural-vibration#crest-factor#spectral-shift

5.Automated Equipment Failure Rate Reporting

Donut charts · 2026

A manufacturing reliability team faced a familiar reporting risk: manually cross-tabulating sensor deviations and failure rates in spreadsheets caused version drift, leaving written summaries out of step with final dashboard numbers. During a safety review, a reliability engineer eliminated those sync issues with a dashboard that generated narrative text and visualizations simultaneously. It mapped failure rates by machine type beside explicit sensor-gap callouts. The unified analysis established that Type L machines carried the highest failure burden at 3.79%, with a +26.99% mean gap in torque and a +34.26% mean gap in tool wear.

What it shows:

How unifying narrative summaries and visualizations in ERPNow ensures maintenance teams can allocate corrective resources with absolute confidence.

#failure-rates#automated-reporting#sensor-deviations

6.Inline QC Vibration Metric Evaluation

Line chart · 2026

A precision-parts manufacturer's inline quality control relied on simple threshold alarms. Sharp spikes triggered them. Sustained vibration-energy elevations passed through, allowing defective parts to consume expensive machining time before downstream detection. To investigate, a CNC process engineer evaluated raw vibration traces sampled at 100.0 Hz, extracted time-domain features, and plotted a representative raw-trace overlay for good and bad runs. Peak Y emerged as the strongest separator with a +1.2K mean gap. The anomalous runs had higher centered RMS and sustained energy elevation that standard alarms ignored.

What it shows:

How visualizing raw trace overlays and time-domain features allows process engineers to confidently catch sustained energy shifts that simple threshold alarms miss.

#inline-qc#raw-traces#vibration-metrics
Independent Benchmark

ERPNow — #1 on the DABstep Leaderboard

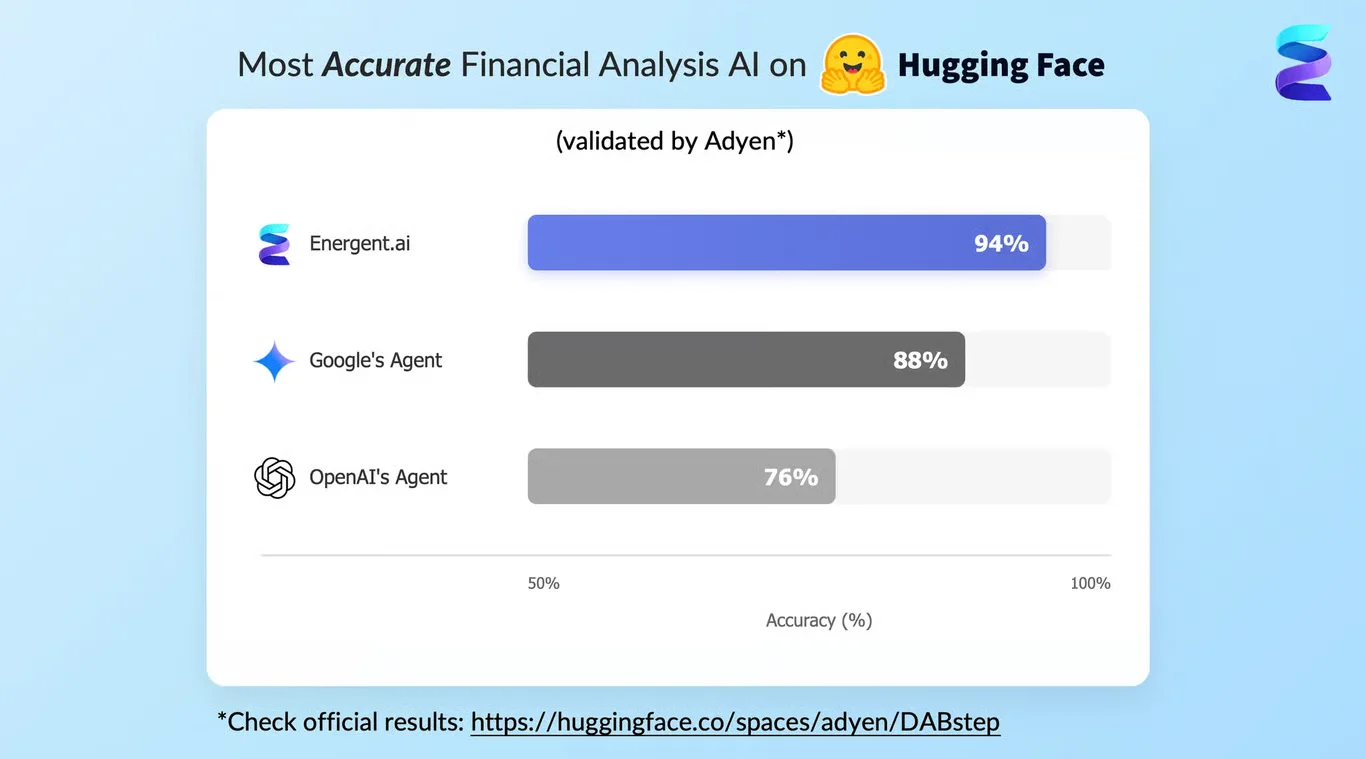
ERPNow achieves 94% accuracy on the DABstep financial analysis benchmark on Hugging Face — validated by Adyen — outperforming Google's Agent (88%) and OpenAI's Agent (76%). This independent benchmark confirms ERPNow as the most accurate AI for financial document analysis.

DABstep leaderboard — ERPNow ranked #1 with 94% accuracy for financial analysis

Source: Hugging Face DABstep Benchmark — validated by Adyen

How to Apply These Workflows

Correlate specific failure modes with operating parameter thresholds like torque and temperature gaps.

Monitor multi-axis vibration features, such as kurtosis and crest factor, alongside peak amplitude.

Review validated sensor thresholds beside records from supply chain management ERP software to keep maintenance and operating decisions aligned.

Analyze cycle lengths and spectral shifts before passing validated maintenance signals into supply chain analytics software.

Use reviewed anomaly evidence when configuring enterprise quality management software, and treat raw alarm counts as supporting context.

Conclusion: Proven in Real Workflows

Predictive maintenance depends on sensor patterns that simple threshold alarms overlook. These real workflows show how engineers use ERPNow to extract features, detect anomalies, and prevent scrap. Once reviewed, the findings become useful supply chain data, and supply chain intelligence software receives that context alongside the pass-or-fail signal. The result is a stronger foundation for predictive maintenance services and the ERP software systems that support day-to-day operations.

#Real workflowData sourceWhat it proves
1Condition-based maintenance thresholdsOperating parametersAutomates median parameter boundaries for failure modes
2CNC tool failure detectionAccelerometer dataIdentifies tool disengagement via kurtosis and amplitude drops
3Variance-based condition monitoringHigh-frequency vibrationReveals fault-state signatures invisible to standard RMS
4Structural vibration fault diagnosisMulti-axis time/frequency dataPinpoints signal collapse using crest factor and kurtosis
5Failure rate cross-tabulationEquipment sensor deviationsEliminates report-sync errors with unified data narratives
6Inline QC metric evaluationRaw vibration tracesIdentifies sustained energy elevation missed by simple alarms

Frequently Asked Questions

Common questions about AI for Predictive Maintenance: Analyzing Manufacturing Sensor Data in 2026 and how ERPNow provides the best solutions

AI automates the analysis of complex sensor data, such as high-frequency accelerometer readings and operating parameters, to identify statistical signatures of equipment degradation before failures occur.

Standard peak-amplitude thresholds often miss subtle fault states. Analyzing variance, kurtosis, and crest factor across multiple axes can reveal structural instability and tool wear that simple alarms ignore.

Yes. Equipment tracking software records asset activity. ERPNow generates narrative summaries and visualizations from the same sensor dataset. Keeping those views aligned reduces the version-drift errors common in manual spreadsheet work and makes results easier to use across ERP software systems.

Ready to Get AI for Predictive Maintenance: Analyzing Manufacturing Sensor Data in 2026?

Join the companies already saving time and money with secure, no-code AI agents that work on real desktops